
In the competitive field of industrial packaging solutions, Hejian Haoyun Plastic Products Factory stands out as a professional manufacturer specializing in injection-molded plastic buckets. Located in Hejian City, Hebei Province, our 5,000-square-meter facility combines advanced production technology with strict quality control to deliver premium packaging solutions for global clients. With a comprehensive product range covering waterproof coating buckets, fire-resistant coating containers, agricultural fertilizer buckets, and specialized chemical storage solutions, we have established ourselves as a trusted partner for businesses across multiple industries.
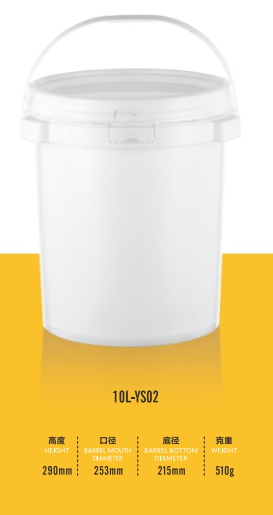
Comprehensive Product Range for Diverse Industrial Needs
Our core product lineup addresses the specific packaging requirements of various industries through specialized designs and material formulations. The waterproof coating bucket series features enhanced moisture resistance and chemical stability, making them ideal for storing architectural coatings, adhesives, and sealants. For fire safety applications, our fire-resistant coating containers undergo rigorous testing to ensure they maintain structural integrity under high-temperature conditions, providing reliable protection for flammable materials during storage and transportation.
The agricultural sector benefits from our durable fertilizer buckets, designed with reinforced walls to withstand rough handling in farming environments while preventing moisture penetration that could compromise product quality. Our bio-agent buckets incorporate anti-corrosion coatings and precise sealing mechanisms to maintain the viability of sensitive biological formulations during long-term storage. For pesticide packaging, we offer UN-certified containers that meet international transportation standards for hazardous materials, ensuring regulatory compliance across global markets.
Special attention has been paid to the automotive care industry with our dedicated car wash liquid buckets. These containers feature impact-resistant construction and ergonomic handles for easy pouring, while the smooth interior surfaces prevent chemical residue buildup. The materials used in these buckets demonstrate excellent resistance to detergents, waxes, and other automotive cleaning agents, ensuring product longevity even with frequent use.
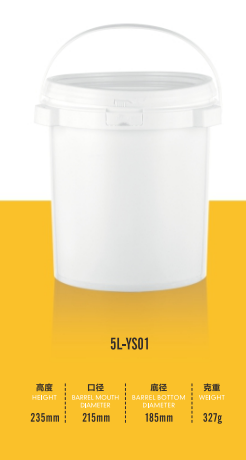
Advanced Manufacturing Capabilities for Custom Solutions
Our production facility represents the pinnacle of modern plastic injection molding technology. Equipped with 12 fully automated production lines and precision molds, we achieve consistent product quality while maintaining high production efficiency. The integration of robotic arms in our assembly processes ensures precise component placement and sealing, minimizing human error and enhancing overall product reliability.
The manufacturing workflow begins with rigorous raw material inspection, where we verify the chemical composition and physical properties of incoming polymers through advanced testing equipment. Our injection molding machines operate with precision temperature control systems to ensure optimal material flow and mold filling, resulting in containers with uniform wall thickness and structural integrity. Each production batch undergoes multiple quality checkpoints, including dimensional verification, pressure testing, and leak detection, before being approved for packaging.
Customization Options for Brand Enhancement
Understanding the importance of brand identity in competitive markets, we offer comprehensive customization services through three advanced printing technologies. In-mold labeling (IML) produces seamless, scratch-resistant graphics that become an integral part of the container surface. Heat transfer printing enables high-definition, multi-color designs with excellent durability against chemicals and abrasion. For cost-effective branding solutions, our screen printing service delivers vibrant, opaque colors even on dark-colored buckets.
Our engineering team collaborates closely with clients to develop custom container designs that optimize storage efficiency and product protection. From ergonomic handle configurations to stackable base designs, we tailor every aspect of the packaging to meet specific application requirements. Volume customization ranges from 5-liter sample containers to 25-liter bulk storage solutions, with intermediate sizes available in 10L, 15L, and 20L configurations to accommodate different product viscosities and usage patterns.
| Product Category | Key Features | Application Fields |
|---|---|---|
| Waterproof Coating Buckets | Moisture-resistant, chemical-stable, UV protection | Architectural coatings, adhesives, sealants |
| Fire-Resistant Containers | High-temperature resistance, flame retardant | Flammable materials storage |
| Agricultural Fertilizer Buckets | Reinforced structure, moisture barrier | Chemical fertilizers, pesticides |
| Bio-Agent Containers | Anti-corrosion, precise sealing | Microbial formulations, enzymes |
| Car Wash Liquid Buckets | Chemical-resistant, ergonomic design | Automotive cleaning products |
Quality Assurance and Environmental Responsibility
Our commitment to quality extends beyond product performance to encompass environmental sustainability throughout the manufacturing process. We have implemented a comprehensive green production system that includes energy-efficient machinery, water recycling systems, and waste reduction programs. All production facilities comply with ISO 14001 environmental management standards, with regular audits ensuring continuous improvement in resource utilization efficiency.
The materials we select for container production meet stringent food-grade safety standards (FDA compliant) while maintaining industrial-grade durability. Our raw material suppliers undergo rigorous qualification processes, with regular batch testing to verify compliance with RoHS and REACH regulations. The injection molding process incorporates closed-loop material recycling systems that reprocess production scrap into new containers, minimizing waste generation and reducing our carbon footprint.
Each finished product undergoes comprehensive performance testing before leaving the factory. Our quality control laboratory is equipped with advanced testing equipment including pressure chambers for leak testing, impact testers for durability verification, and environmental chambers for accelerated aging simulations. These rigorous testing protocols ensure that every container leaving our facility can withstand the rigors of transportation, storage, and end-use conditions while maintaining product integrity.
FAQ
What customization options are available for plastic buckets?
We offer comprehensive customization services including volume adjustments from 5L to 25L, color matching to corporate branding, and three printing technologies: in-mold labeling for seamless graphics, heat transfer printing for high-definition multi-color designs, and screen printing for cost-effective branding. Our engineering team can also develop custom handle designs, stacking features, and dispensing systems based on specific application requirements.
How does your factory ensure product quality consistency?
Quality control is integrated at every stage of production through automated inspection systems and manual verification processes. Raw materials undergo composition analysis before use, while production parameters are continuously monitored by PLC systems. Each finished container passes through multiple checkpoints including dimensional verification, pressure testing, and leak detection. Our ISO 9001 certified quality management system ensures consistent adherence to international standards across all production batches.
What certifications do your industrial containers have?
Our product range holds multiple international certifications including FDA food contact approval, UN certification for hazardous materials transportation, and RoHS compliance for restricted substances. The manufacturing facility maintains ISO 9001 quality management and ISO 14001 environmental management certifications, with regular third-party audits to ensure ongoing compliance with global regulatory requirements for industrial packaging solutions.
How do you handle bulk orders and production lead times?
With 12 fully automated production lines, our monthly capacity exceeds 500,000 units across all container sizes. Standard orders typically ship within 15-20 working days after sample approval, with expedited production available for urgent requests. For new customers, we offer free sample production within 5 working days to verify product specifications before full-scale manufacturing. Our port-direct shipping service from Tianjin Xingang Port ensures efficient global distribution.
What makes your agricultural chemical containers different from competitors?
Our agricultural containers feature triple-layer construction with UV protection coating, reinforced wall structure, and specialized sealing systems designed for harsh farming environments. The materials demonstrate excellent resistance to common agricultural chemicals including ammonia-based fertilizers, sulfur pesticides, and acidic soil amendments. Each container undergoes 72-hour chemical compatibility testing to ensure zero degradation when storing specific formulations.
Summary
Hejian Haoyun Plastic Products Factory has established itself as a premier manufacturer of industrial plastic containers through technical innovation, rigorous quality control, and customer-centric service. Our comprehensive product range addresses the packaging challenges of diverse industries with specialized designs that optimize product protection, storage efficiency, and brand presentation. With advanced manufacturing capabilities, comprehensive customization options, and a strong commitment to environmental sustainability, we continue to set industry benchmarks for quality and reliability in industrial packaging solutions.