
In today’s competitive industrial landscape, the right packaging solution can make all the difference in product safety, transportation efficiency, and brand reputation. HeYun Plastic, a leading manufacturer based in Hejian City, China, specializes in creating high-quality custom plastic buckets that meet the diverse needs of global industries. With over 5,000 square meters of modern production facilities and advanced injection molding equipment, we deliver durable, corrosion-resistant containers designed for specific applications across multiple sectors.
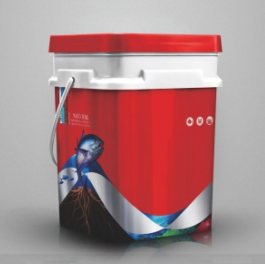
Core Product Range: Specialized Solutions for Every Industry
Our comprehensive product portfolio addresses the packaging challenges of various sectors through six main categories of specialized plastic buckets:
1. Waterproof Coating Plastic Buckets
Engineered specifically for the construction industry, our waterproof coating buckets feature exceptional chemical resistance and airtight sealing mechanisms. The smooth interior surface prevents material adhesion, while the reinforced rim structure withstands repeated opening and closing during construction projects. These buckets are available in capacities ranging from 5L to 30L, with optional tamper-evident lids for added security during transportation.
2. Fireproof Coating Packaging Buckets
For fire-retardant material storage, our fireproof coating buckets incorporate flame-retardant additives in the plastic formulation while maintaining all the durability benefits of standard polyethylene. The double-wall design provides thermal insulation, protecting contents from temperature fluctuations during storage and transport. These containers meet international fire safety standards, making them ideal for global distribution of fireproof coatings.
3. Agricultural Fertilizer Plastic Buckets
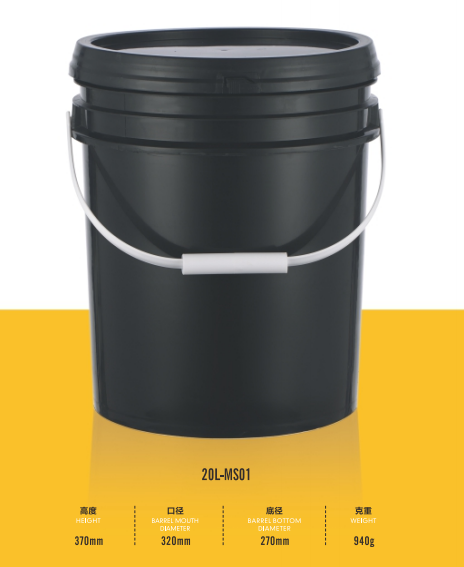
Our agricultural solutions address the unique challenges of fertilizer storage and transportation. These UV-stabilized buckets resist degradation from sunlight exposure, while the anti-static formulation prevents dust accumulation during handling. The ergonomic handle design reduces operator fatigue during field applications, and the graduated measurement markings enable precise dosage control. We offer both open-top and screw-cap versions to suit different fertilizer formulations.
4. Biological Agent Packaging Buckets
For sensitive biological products, our specialized containers feature sterile production environments and medical-grade plastic formulations. The airtight sealing system maintains product viability during storage, while the opaque exterior protects light-sensitive contents. These buckets comply with international bio-safety standards and can be sterilized through multiple methods including gamma irradiation and ethylene oxide treatment.
Advanced Manufacturing Capabilities
At HeYun Plastic, we combine cutting-edge technology with rigorous quality control to deliver packaging solutions that exceed industry expectations. Our fully automated production lines utilize high-precision injection molding machines capable of maintaining tolerances within ±0.1mm across all dimensions. This precision ensures consistent product quality batch after batch, which is critical for applications requiring exact container specifications.
Our quality management system follows ISO 9001:2015 standards, with comprehensive testing protocols at every production stage:
- Raw material inspection for purity and consistency
- In-process monitoring of wall thickness and dimensional accuracy
- Drop testing from 1.2 meters height to verify impact resistance
- Leak testing under 0.5 bar pressure for 24 hours
- Final inspection of sealing performance and surface finish
The table below illustrates our standard production parameters for different bucket types:
| Parameter | Waterproof Coating Bucket | Agricultural Fertilizer Bucket | Biological Agent Bucket |
|---|---|---|---|
| Material Grade | HDPE with chemical additives | UV-stabilized HDPE | Medical-grade PP |
| Wall Thickness | 2.5-3.0mm | 2.0-2.5mm | 3.0-3.5mm |
| Temperature Range | -40°C to +60°C | -30°C to +50°C | -20°C to +40°C |
| Stacking Test | 5 layers for 24 hours | 4 layers for 24 hours | 3 layers for 24 hours |
Customization Capabilities: Tailored Solutions for Unique Requirements
Understanding that standard products cannot meet all industrial needs, we offer comprehensive customization services through our advanced design and engineering capabilities. Our team works closely with clients from concept development to final production, ensuring the packaging solution perfectly matches their requirements.
Key customization options include:
- Dimensional Customization: From 1L to 50L capacities with precise height-diameter ratios optimized for specific storage spaces
- Material Selection: Choice of HDPE, LDPE, PP, or engineered plastics with special additives for UV resistance, anti-static properties, or food-grade compliance
- Color Matching: Precise Pantone color matching for brand consistency, with options for opaque, translucent, or transparent formulations
- Labeling Solutions: In-mold labeling (IML) for permanent branding, heat transfer printing for high-resolution graphics, or silk-screen printing for cost-effective solutions
- Functional Add-ons: Integrated handles, pouring spouts, measurement markings, tamper-evident features, or child-resistant closures
Our design process begins with a detailed consultation to understand your specific needs, followed by 3D modeling and prototype production for functional testing. This iterative approach ensures the final product meets all performance requirements before full-scale production begins.
Global Compliance and Certifications
As an international supplier, we recognize the importance of meeting diverse regulatory requirements across different markets. Our quality management system is certified to ISO 9001:2015 standards, and we maintain compliance with major international regulations including:
- FDA food contact compliance (21 CFR Part 177.1520) for food-grade containers
- UN certification for hazardous materials packaging (when required)
- REACH compliance for chemical substances in the European market
- RoHS directive compliance for restricted substances in electrical applications
- GMP standards for pharmaceutical and biological agent packaging
We provide comprehensive documentation with each shipment, including material certificates, testing reports, and compliance declarations, to facilitate smooth customs clearance and regulatory approval in your destination market.
FAQ
What makes your plastic buckets suitable for chemical storage?
Our chemical storage buckets use high-density polyethylene (HDPE) with special additives that enhance chemical resistance against acids, alkalis, and solvents. The production process includes rigorous testing for permeability and reaction with common industrial chemicals, ensuring safe containment for at least 12 months under normal storage conditions.
How do you ensure consistent quality across large production batches?
We implement multiple quality control measures including: 1) Automated material feeding systems that maintain precise additive ratios, 2) In-line sensors that monitor wall thickness during molding, 3) Statistical process control (SPC) software that tracks production parameters in real-time, and 4) Random sampling inspection of finished products against our quality standards.
What customization options are available for branding my products?
We offer three main branding solutions: In-mold labeling (IML) for permanent, high-resolution graphics that become part of the container; Heat transfer printing for complex multi-color designs with excellent durability; and Silk-screen printing for cost-effective single-color branding. All methods comply with food safety standards when required.
How do you handle urgent orders or small batch production?
Our flexible production system can accommodate urgent orders through dedicated production lines and optimized scheduling. For small batches (minimum order quantity starts at 500 pieces for custom designs), we use quick-change molds and streamlined setup processes to maintain efficiency while meeting your delivery deadlines.
Summary
HeYun Plastic stands as a trusted partner for industrial packaging solutions, combining advanced manufacturing technology with deep industry expertise to deliver containers that protect, preserve, and present your products effectively. Our comprehensive range of standard products, coupled with extensive customization capabilities, ensures we can meet the unique requirements of any application across construction, agriculture, chemicals, and beyond.
With a commitment to quality that begins with raw material selection and extends through final inspection, we provide packaging solutions that enhance your product value while reducing total cost of ownership through durability and reliability. Our global compliance expertise further ensures seamless market access wherever your business operates.
For businesses seeking a packaging partner that understands both the technical requirements and commercial realities of industrial containers, HeYun Plastic offers the perfect combination of innovation, quality, and service. Contact our team today to discuss how we can help optimize your packaging strategy for better performance and greater market success.