
In the competitive global market for industrial packaging solutions, Hejian Haoyun Plastic Factory stands out as a premier manufacturer specializing in high-quality plastic buckets for various applications. With over 5,000 square meters of modern production facilities in Hejian City, Hebei Province, our company combines advanced technology with strict quality control to deliver superior packaging solutions to clients worldwide.
Our product range includes specialized containers for pesticide and fertilizer storage, waterproof and fireproof coating buckets, agricultural chemical containers, biological agent packaging, car wash liquid containers, and more. Each product is engineered to meet the specific demands of different industries while maintaining our core values of durability, safety, and environmental responsibility.
Advanced Manufacturing Capabilities
At Hejian Haoyun Plastic Factory, we invest heavily in state-of-the-art production equipment to ensure consistent quality across all our products. Our facility features international-standard injection molding machines, fully automated production lines, and precision molds that enable efficient, large-scale manufacturing with minimal variation between batches.
The production process begins with rigorous raw material selection. We only use premium-grade polymers that meet international food safety and chemical resistance standards. Our quality control team conducts comprehensive testing on incoming materials to verify their purity and performance characteristics before they enter production.
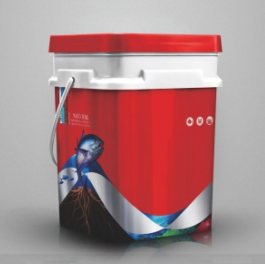
During manufacturing, we employ advanced techniques including in-mold labeling (IML), heat transfer printing, and screen printing to create professional, durable branding on each container. These processes ensure that logos and product information remain clear and legible throughout the product’s service life, even when exposed to harsh chemicals or environmental conditions.
Product Features and Advantages
Our plastic buckets are designed with multiple performance characteristics that make them ideal for demanding industrial applications:
- Lightweight Durability: Constructed from high-density polyethylene (HDPE) or polypropylene (PP), our buckets offer excellent strength-to-weight ratios, reducing transportation costs while maintaining structural integrity.
- Corrosion Resistance: Special formulations resist degradation from acids, alkalis, solvents, and other chemicals commonly found in agricultural and industrial settings.
- Impact Resistance: Engineered to withstand drops and impacts during handling and transportation without cracking or deforming.
- Sealing Performance: Precision-molded lids and gaskets create airtight seals that prevent leakage and protect contents from moisture and contaminants.
- Temperature Tolerance: Capable of withstanding extreme temperatures from -40°C to 80°C without losing dimensional stability.
- UV Stability: Optional UV inhibitors protect contents from sunlight degradation for outdoor storage applications.
Customization Options
Understanding that different industries have unique packaging requirements, we offer comprehensive customization services:
| Customization Aspect | Available Options |
|---|---|
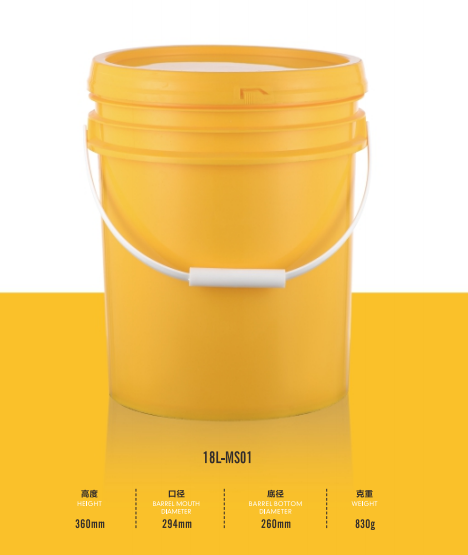
| Capacity | 1L to 50L standard sizes, custom volumes available |
| Dimensions | Custom diameter and height to fit specific storage or transportation requirements |
| Color | Standard colors or custom Pantone matching |
| Printing | Multi-color screen printing, heat transfer, or in-mold labeling with custom logos and text |
| Handles | Integrated or attached handles in various designs for ergonomic carrying |
| Accessories | Custom lids, spouts, measuring scales, or other functional additions |
Quality Assurance System
Our commitment to quality extends throughout the entire production process and supply chain. We maintain certification to ISO 9001:2015 quality management standards and implement comprehensive quality control measures at every stage:
Raw Material Inspection: Each batch of polymers undergoes testing for purity, melt flow rate, density, and other critical parameters before being approved for production.
In-Process Quality Control: Automated monitoring systems track production parameters in real-time, while quality inspectors conduct periodic checks on dimensions, wall thickness, and surface finish.
Finished Product Testing: Random samples from each production run undergo rigorous performance testing including drop tests, seal integrity tests, and chemical compatibility tests.
Packaging Inspection: Before shipping, all products are visually inspected for printing quality, packaging integrity, and proper labeling according to customer specifications and international regulations.
Application Industries
The versatility and durability of our plastic buckets make them suitable for a wide range of industries:
- Agriculture: Storage and transportation of pesticides, fertilizers, herbicides, and other agricultural chemicals
- Construction: Packaging for waterproof coatings, fireproof materials, adhesives, and sealants
- Chemical Processing: Safe containment of industrial solvents, cleaning agents, and raw materials
- Food Industry: Storage of edible oils, sauces, and other food-grade liquids (when using food-grade approved materials)
- Automotive: Packaging for car wash chemicals, lubricants, and maintenance fluids
- Pharmaceutical: Storage of biological agents and pharmaceutical intermediates (under specific material approvals)
- Logistics: General-purpose containers for warehouse storage and material handling
FAQ
What makes your plastic buckets suitable for storing aggressive chemicals?
Our buckets are manufactured using high-density polyethylene (HDPE) or polypropylene (PP) specifically formulated for chemical resistance. These materials demonstrate excellent stability when exposed to acids, alkalis, solvents, and other aggressive substances commonly found in agricultural and industrial settings. Additionally, we can customize the material formulation based on specific chemical compatibility requirements.
How do you ensure the printing quality on custom-labeled buckets?
We employ three advanced printing technologies: in-mold labeling (IML) for the most durable finish, heat transfer printing for high-resolution multi-color designs, and screen printing for cost-effective single-color applications. All printing processes are performed using UV-resistant inks and undergo rigorous adhesion testing to ensure logos and text remain clear and intact throughout the product’s service life.
What certifications do your products hold for international markets?
Our manufacturing facility maintains ISO 9001:2015 certification for quality management systems. Many of our products comply with international standards including FDA food contact regulations (when using food-grade materials), UN transportation regulations for dangerous goods packaging, and REACH/RoHS environmental standards. We can provide specific compliance documentation upon request for each product type.
Can you produce buckets with specific color requirements for brand consistency?
Absolutely. We offer standard color options from our color library and can match any custom Pantone color for minimum order quantities. Our color matching process uses computerized spectrophotometers to ensure precise color reproduction batch after batch, maintaining consistent brand appearance across all your packaging.
What is your minimum order quantity for custom printed buckets?
Our minimum order quantity varies depending on the bucket size and printing method. For standard sizes with screen printing, we typically require a minimum of 500-1,000 pieces per design. For in-mold labeling or more complex customizations, the MOQ may be higher. We work closely with clients to find solutions that balance their branding needs with cost-effective production.
Summary
Hejian Haoyun Plastic Factory has established itself as a trusted partner for businesses worldwide seeking high-quality, reliable plastic packaging solutions. Our commitment to advanced manufacturing technology, rigorous quality control, and comprehensive customization services ensures that we can meet the most demanding requirements across diverse industries.
With a product range specifically designed for chemical storage, agricultural applications, and industrial use, our plastic buckets offer the perfect combination of durability, safety, and functionality. Our ability to provide custom printing and branding solutions helps clients enhance their product presentation while maintaining compliance with international packaging regulations.
As we look to the future, Hejian Haoyun remains dedicated to continuous improvement in both product performance and environmental responsibility. We are constantly exploring new materials and production methods to reduce our environmental footprint while delivering even more value to our customers. Contact us today to discuss how we can support your packaging needs with our premium plastic bucket solutions.