
In the industrial packaging sector, the demand for reliable, durable, and customizable plastic containers continues to grow across various sectors including chemicals, agriculture, food processing, and logistics. HeYun Plastic Factory, located in Hejian City, Hebei Province, has established itself as a leading manufacturer specializing in injection-molded plastic buckets that meet the stringent requirements of modern industrial applications. With a 5,000-square-meter production facility equipped with advanced automation systems and precision molds, we deliver high-performance packaging solutions tailored to global clients’ specific needs.
Core Product Advantages
Our injection-molded plastic buckets offer several competitive advantages that make them ideal for demanding industrial environments. First, the material selection focuses on high-density polyethylene (HDPE) and polypropylene (PP) that provide excellent chemical resistance, preventing corrosion from various substances including acids, alkalis, and solvents. This chemical stability ensures product safety during storage and transportation of agricultural chemicals, industrial coatings, and cleaning agents.
The structural design incorporates reinforced rims and thickened walls to achieve superior impact resistance. Our testing shows these buckets can withstand drops from 1.5 meters without deformation or cracking, making them suitable for rough handling in logistics centers and construction sites. The seamless construction eliminates weak points, while the precision-molded lids create airtight seals that prevent leakage and contamination.
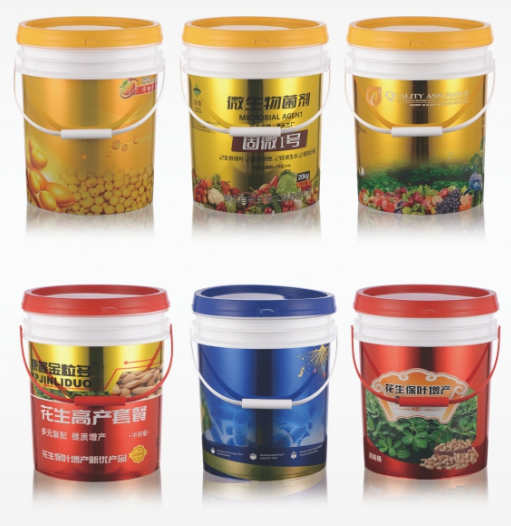
For applications requiring specific identification or branding, we offer multiple customization options. In-mold labeling (IML) technology permanently fuses labels during the molding process, creating scratch-resistant graphics that withstand harsh environments. Thermal transfer printing enables high-resolution, multi-color designs for product information and branding. Screen printing remains a cost-effective solution for simple yet durable markings.
Industry-Specific Applications
The versatility of our plastic buckets supports diverse industrial requirements. In the agricultural sector, our fertilizer buckets feature UV stabilization to prevent degradation from sunlight exposure during outdoor storage. The smooth interior surfaces facilitate easy cleaning between different fertilizer types, while the standardized dimensions ensure compatibility with existing handling equipment.
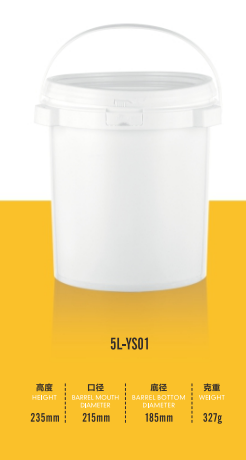
For chemical manufacturers, our corrosion-resistant buckets meet international packaging standards for hazardous materials transportation. The optional UN certification ensures compliance with global regulations for shipping dangerous goods by road, rail, or sea. The ergonomic handle design reduces operator fatigue during repeated handling of heavy containers.
The food processing industry benefits from our FDA-compliant buckets that maintain product purity during storage and transportation. The non-porous material prevents bacterial growth, while the tight-fitting lids protect contents from external contaminants. These buckets are widely used for storing edible oils, food additives, and powdered ingredients.
Technical Specifications Comparison
Our product range includes multiple capacities and configurations to suit different applications:
| Capacity | Material Grade | Wall Thickness | Certifications |
|---|---|---|---|
| 5L-10L | Food-grade HDPE | 2.5mm-3.0mm | FDA, EU 10/2011 |
| 15L-25L | Industrial HDPE | 3.5mm-4.0mm | UN, RoHS |
| 30L-50L | Chemical-resistant PP | 4.5mm-5.0mm | ISO 9001, SGS |
Production Capabilities & Quality Control
Our fully automated production lines enable efficient mass production while maintaining consistent quality. The injection molding process uses computer-controlled parameters to ensure each bucket meets precise dimensional tolerances within ±0.5mm. The in-line quality inspection system automatically rejects any containers with surface defects or structural weaknesses.
The quality management system follows ISO 9001 standards with comprehensive testing procedures at each production stage. Raw materials undergo chemical composition analysis before use, while finished products pass drop tests, leak tests, and stacking tests. Our laboratory equipment includes spectrometers for material analysis, pressure chambers for seal testing, and environmental chambers for aging simulation.
For customized orders, our engineering team collaborates closely with clients to develop optimal solutions. This includes 3D modeling of proposed designs, prototype production, and field testing in actual working conditions. The modular mold system allows cost-effective production of small batches with quick turnaround times.
FAQ
What materials do you use for chemical-resistant buckets?
We primarily use high-density polyethylene (HDPE) and polypropylene (PP) for our chemical-resistant containers. HDPE offers excellent resistance to acids, alkalis, and solvents, while PP maintains stability at higher temperatures. For specific applications requiring additional resistance, we can incorporate specialized additives during the molding process.
Can you produce buckets with UN certification for hazardous materials?
Yes, we offer UN-certified buckets that comply with international regulations for transporting dangerous goods. These containers undergo rigorous testing including drop tests, stack tests, and leak tests to meet packaging group requirements. The certification marks are permanently molded into each container along with the batch number for traceability.
What customization options are available for branding?
We provide three main branding solutions: in-mold labeling (IML) for permanent, high-resolution graphics; thermal transfer printing for detailed multi-color designs; and screen printing for cost-effective simple markings. All methods produce durable results that withstand industrial handling and environmental exposure.
How do you ensure consistent quality across large orders?
Our fully automated production lines use computer-controlled injection molding machines with precise parameter settings. Each machine produces containers with consistent wall thickness and dimensional accuracy. The in-line quality inspection system automatically checks every item for defects, while random sampling undergoes additional laboratory testing.
What is the minimum order quantity for custom designs?
The minimum order quantity depends on the complexity of the customization. For simple color changes or standard label designs, we can accommodate orders starting from 500 units. For completely new mold designs or specialized material formulations, the MOQ typically ranges from 1,000 to 2,000 units depending on the container size.
Summary
HeYun Plastic Factory combines advanced manufacturing technology with rigorous quality control to deliver industrial plastic buckets that meet the most demanding requirements. Our product range covers various capacities and material grades suitable for chemical storage, agricultural applications, food processing, and general industrial use. With comprehensive customization options and certifications for international markets, we help clients enhance their packaging efficiency while maintaining product safety and brand integrity. The fully automated production system ensures consistent quality at competitive pricing, supported by our professional team’s technical expertise and responsive service.