
In the global industrial packaging market, the demand for high-quality, customized plastic containers continues to grow across various sectors including chemicals, agriculture, food processing, and logistics. As a professional manufacturer with over 5000 square meters of modern production facilities in Hejian City, Hebei Province, Hejian Haoyun Plastic Factory has established itself as a trusted partner for businesses seeking reliable industrial packaging solutions. Specializing in injection-molded plastic buckets ranging from coating containers to agricultural storage drums, our company combines advanced manufacturing technology with stringent quality control to deliver products that meet international standards.
Comprehensive Product Range for Diverse Industrial Needs
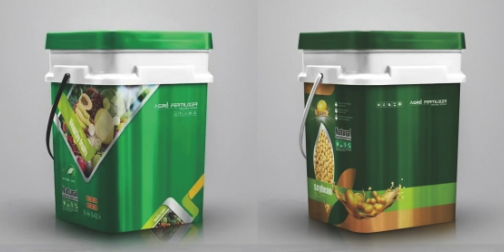
Our product portfolio covers six main categories of industrial plastic buckets, each designed to address specific packaging requirements across different industries. The waterproof coating buckets feature specialized sealing mechanisms that prevent moisture ingress, making them ideal for storing architectural coatings, adhesives, and other moisture-sensitive materials. For fire-resistant applications, our fireproof coating buckets incorporate flame-retardant materials and reinforced structures that maintain container integrity even under high-temperature conditions.
In the agricultural sector, our fertilizer buckets and biological agent containers are engineered to withstand the corrosive nature of chemical fertilizers and microbial formulations. The agricultural-grade plastic we use demonstrates excellent resistance to ammonia, urea, and other common agricultural chemicals, ensuring product longevity even with prolonged storage. For pesticide applications, our dedicated pesticide buckets feature dual-layer construction with UV protection to prevent chemical degradation while maintaining operator safety through ergonomic handle designs and spill-proof lids.
The automotive industry benefits from our specialized car wash liquid buckets that combine chemical resistance with transparent level indicators for accurate dosing. These containers undergo rigorous testing against common car care chemicals including wax removers, tire shiners, and glass cleaners to ensure compatibility without material degradation or color transfer.
Advanced Manufacturing Capabilities for Custom Solutions
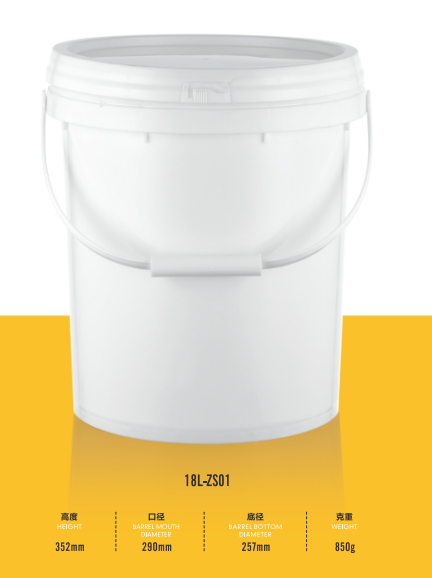
At the core of our production system lies a fully automated injection molding line equipped with precision molds from leading European manufacturers. This investment in advanced equipment enables us to maintain consistent wall thickness across all containers, eliminate weak points that could lead to cracking, and achieve dimensional accuracy within ±0.5mm tolerance. Our 128-cavity molds allow for high-volume production without compromising quality, with daily output capacity exceeding 20,000 units during peak periods.
The manufacturing process incorporates several quality control checkpoints beginning with raw material inspection. We exclusively use virgin polyethylene (PE) and polypropylene (PP) compounds that meet FDA standards for food contact applications, ensuring our containers are safe for storing edible oils, dairy products, and other food items. Each batch of raw materials undergoes spectral analysis to verify chemical composition before entering production.
During molding, our computerized systems monitor cavity pressure, injection speed, and cooling time to optimize part formation. This data-driven approach minimizes internal stresses that could affect container durability. Post-molding, every bucket passes through automated leak detection equipment that applies 0.5 bar pressure to check for microscopic defects invisible to the naked eye. Only containers that maintain pressure for 30 seconds without leakage proceed to final inspection.
Customization Options for Brand Enhancement
Understanding the importance of brand identity in competitive markets, we offer comprehensive customization services through three primary decoration technologies. In-mold labeling (IML) provides the most durable branding solution by embedding labels directly into the container wall during molding, creating a seamless surface that resists peeling and abrasion. This method is particularly popular for high-volume runs where consistent brand presentation is critical.
For smaller batches or frequent design changes, our thermal transfer printing technology offers excellent print quality with vibrant colors and fine details. This digital printing method allows for quick turnaround times and cost-effective production of multi-color designs without the need for expensive printing plates. Screen printing remains the preferred choice for simple, bold designs requiring maximum opacity and chemical resistance, particularly for industrial containers exposed to harsh environments.
Our engineering team works closely with clients to develop custom container designs that optimize storage efficiency and product protection. This includes specialized shapes for space-saving stacking, reinforced handles for heavy loads, and tamper-evident features for security-sensitive products. We also offer color matching services to ensure container appearance aligns perfectly with client branding guidelines.
| Product Category | Capacity Range | Material Grade | Certification |
|---|---|---|---|
| Waterproof Coating Buckets | 5L-25L | HDPE (Food Grade) | FDA, RoHS |
| Agricultural Fertilizer Buckets | 10L-50L | Chemical-Resistant PP | UN Approved |
| Pesticide Storage Containers | 3L-20L | UV-Stabilized HDPE | ISO 9001 |
| Food Processing Buckets | 2L-15L | Virgin PE | FDA, EU 10/2011 |
FAQ
What certifications do your industrial plastic buckets hold?
Our containers comply with multiple international standards including FDA food contact approval, RoHS environmental compliance, and UN packaging certification for hazardous materials transport. All products undergo regular third-party testing by SGS and Intertek to verify compliance with destination market requirements. For food-grade containers, we maintain HACCP certification and provide detailed material traceability reports upon request.
How do you ensure consistent quality across large production runs?
Quality control begins with our automated material handling system that prevents contamination between different resin batches. During production, our computerized injection molding machines maintain precise process parameters with real-time monitoring of cavity pressure, injection speed, and cooling cycles. Each container passes through automated leak detection and dimensional inspection before final packaging, with statistical process control (SPC) charts generated for every production shift to identify potential quality trends early.
What customization options are available for branding our containers?
We offer three primary decoration methods: In-mold labeling for high-volume, durable branding; thermal transfer printing for vibrant multi-color designs with quick turnaround; and screen printing for cost-effective single-color applications. Our design team can assist with artwork adaptation to ensure optimal print results on curved container surfaces, and we maintain Pantone color matching capabilities to maintain brand consistency across all packaging materials.
How do your containers perform in extreme temperature conditions?
Our standard containers withstand temperatures from -40°C to +60°C without deformation or material degradation. For applications requiring broader temperature ranges, we offer specialized formulations using high-performance polymers that maintain functionality from -50°C to +80°C. These extreme-temperature containers feature reinforced structures and specialized sealing systems to prevent leakage under thermal stress.
Summary
As a leading manufacturer of industrial plastic containers, Hejian Haoyun Plastic Factory combines advanced production technology with rigorous quality control to deliver packaging solutions that meet the most demanding requirements across diverse industries. Our comprehensive product range covers everything from food-grade containers to chemical-resistant drums, all manufactured using virgin materials that comply with international safety standards. With full customization capabilities including size, shape, color, and branding options, we empower clients to create distinctive packaging that enhances product value while ensuring safe storage and transportation. Our commitment to continuous improvement in both product performance and environmental sustainability positions us as the preferred partner for businesses seeking reliable, high-quality industrial packaging solutions.