
When it comes to industrial packaging solutions, selecting the right plastic bucket is crucial for product safety, transportation efficiency, and brand reputation. As a professional manufacturer with over 5,000 square meters of modern production facilities in Hejian, Hebei Province, Hejian Haoyun Plastic specializes in developing high-quality plastic packaging containers that meet diverse industry requirements. This comprehensive guide will walk you through everything you need to know about selecting industrial plastic buckets, with insights from our 15+ years of manufacturing experience.
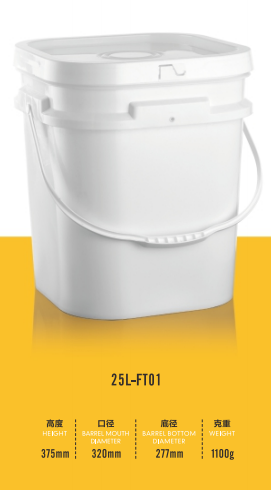
Understanding Your Packaging Requirements
The first step in selecting industrial plastic buckets is to clearly define your specific needs. Different industries have unique requirements that impact bucket selection:
Chemical Industry Applications
For waterproof and fireproof coating manufacturers, the buckets must withstand chemical corrosion while maintaining structural integrity. Our waterproof coating plastic buckets feature specialized resin formulations that resist solvent penetration and prevent container degradation over time. The fireproof coating packaging buckets undergo rigorous flame-retardant testing to meet international safety standards.
Agricultural Sector Needs
Agricultural chemical packaging presents distinct challenges. Our agricultural fertilizer buckets and pesticide containers are designed with:
- UV-resistant materials for outdoor storage
- Child-resistant locking mechanisms for safety
- Chemical-compatible liners to prevent interaction
- Precise measurement markings for accurate dosing
The bio-agent buckets for microbial fertilizers incorporate special ventilation systems to maintain product viability during storage and transportation. Each container undergoes pressure testing to ensure zero leakage under normal handling conditions.
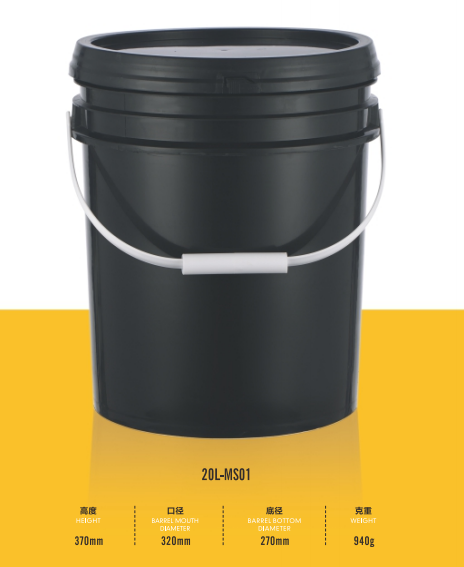
Key Selection Criteria for Industrial Plastic Buckets
When evaluating different suppliers and product options, consider these essential factors that determine bucket performance and reliability:
Material Quality and Composition
The base material significantly impacts bucket durability. We use food-grade HDPE (High-Density Polyethylene) for most containers, which offers:
- Excellent impact resistance (drop tests from 2 meters)
- Chemical inertness to withstand 98% of industrial chemicals
- Temperature resistance from -40°C to 80°C
- 100% recyclable material meeting global sustainability standards
For specialized applications, we offer PP (Polypropylene) buckets with higher heat resistance and PET containers for transparent packaging needs. All materials comply with FDA and EU food contact regulations.
Manufacturing Process Standards
The production method directly affects container consistency and quality. Our fully automated injection molding lines ensure:
- Uniform wall thickness (±0.2mm tolerance)
- Precise dimensional control (±1mm on critical dimensions)
- Elimination of human error in production
- Batch-to-batch consistency for reliable performance
Each production run includes statistical process control (SPC) monitoring and regular material property testing to maintain quality standards.
| Testing Parameter | Acceptance Criteria | Testing Method |
|---|---|---|
| Drop Impact | No cracking at 2m drop | ASTM D2463 |
| Seal Integrity | Zero leakage at 0.3bar | Internal Method |
| Chemical Resistance | No swelling >5% | ASTM D543 |
Customization Options for Specialized Needs
One of our core strengths as a manufacturer is the ability to create tailored solutions for unique packaging requirements. Our customization capabilities include:
Structural Modifications
Beyond standard sizes (5L to 50L), we can design containers with:
- Special handles for ergonomic carrying
- Integrated measurement scales
- Stacking ribs for stable palletization
- UN-certified designs for hazardous materials
For automotive coating manufacturers, we developed a square bucket with reinforced corners that reduces pallet space usage by 18% compared to round containers.
Branding and Identification Solutions
Our in-house decoration capabilities help enhance brand visibility:
- In-mold labeling (IML) for 360° branding
- Hot stamping for metallic finishes
- Silk-screen printing with food-grade inks
- RFID tag integration for supply chain tracking
For a European agricultural chemical company, we implemented a color-coding system with IML technology that reduced product mix-ups by 92% in distribution centers.
FAQ
What certifications should I look for in industrial plastic buckets?
Reputable manufacturers should provide testing reports for key standards including UN certification for dangerous goods, FDA food contact compliance, and ISO 9001 quality management. Our products carry all necessary certifications for global market access.
How do I determine the right bucket size for my products?
Consider both volume requirements and handling efficiency. We recommend selecting the smallest container that safely holds your product volume while allowing 10-15% headspace for expansion. Our engineers can provide optimal sizing recommendations based on your specific application.
What’s the typical lead time for custom bucket orders?
For standard products from our inventory, we can ship within 7 days. Custom orders typically require 4-6 weeks from design approval to production completion, depending on complexity. We maintain strategic raw material stock to expedite custom projects.
How does your quality control process ensure consistent bucket performance?
We implement a 5-stage quality assurance system: incoming material inspection, in-process quality checks, finished product testing, random sampling for aging tests, and pre-shipment verification. Each container has a traceable production code for quality tracking.
Summary
Selecting the right industrial plastic buckets requires careful consideration of material properties, manufacturing standards, and application-specific requirements. As a professional manufacturer with ISO-certified facilities and 15+ years of industry experience, Hejian Haoyun Plastic offers comprehensive solutions from standard containers to fully customized packaging systems. Our commitment to quality is demonstrated through rigorous testing protocols, advanced production technology, and responsive customer service. Whether you need waterproof coating buckets, fireproof packaging containers, or specialized agricultural chemical containers, we have the expertise and capabilities to deliver packaging solutions that protect your products and enhance your brand value.