
In the global industrial packaging market, the demand for high-quality, customized plastic containers continues to grow across sectors including chemicals, agriculture, food processing, and logistics. Hejian Haoyun Plastic Factory, located in Hejian City, Hebei Province, has established itself as a premier manufacturer specializing in injection-molded plastic buckets since its inception. With a 5,000-square-meter production facility equipped with advanced automated systems and precision molds, the company delivers comprehensive packaging solutions that meet international quality standards while addressing diverse industry requirements.
Core Product Advantages
The company’s flagship product line comprises specialized plastic buckets engineered for demanding industrial environments. These containers demonstrate exceptional resistance to corrosion, impact, and temperature variations while maintaining lightweight characteristics for efficient handling. The material selection process prioritizes food-grade and chemical-resistant polymers that comply with FDA and EU safety regulations, ensuring suitability for storing everything from agricultural fertilizers to industrial solvents.
Each bucket undergoes rigorous quality control through 12 production stages, including:
- High-precision injection molding with tolerance control within ±0.1mm
- Automated leak testing under 0.5 bar pressure for 24 hours
- UV stabilization treatment for outdoor applications
- Impact resistance testing from 1.5-meter drops onto concrete surfaces
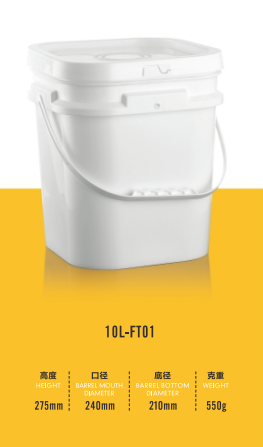
The production facility operates 24 fully automated lines capable of producing 120,000 units monthly across 15 standard sizes ranging from 5L to 50L capacity. This scale enables cost-effective bulk production while maintaining consistent quality through computerized process monitoring and real-time defect detection systems.
Customization Capabilities
Understanding the diverse needs of global clients, Hejian Haoyun offers comprehensive customization services that extend beyond dimensional adjustments. The engineering team collaborates with customers to develop tailored solutions incorporating:
Material Selection
Clients can choose from multiple polymer grades including:
- HDPE for chemical resistance (pH 2-12)
- PP for high-temperature applications (up to 120°C)
- Food-grade LDPE for edible product packaging
- UV-stabilized variants for outdoor storage
Functional Enhancements
The design team implements specialized features such as:
- Tamper-evident seals for pharmaceutical applications
- UN-certified designs for hazardous material transport
- Stacking ribs for optimized warehouse space utilization
- Ergonomic handles with anti-slip textures
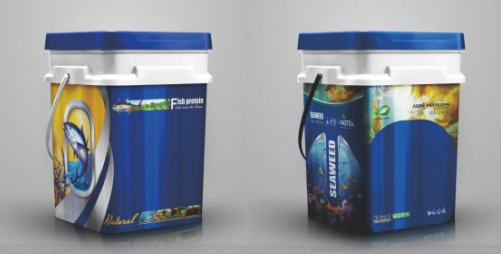
Branding Solutions
Three professional decoration methods ensure brand visibility:
| Method | Application | MOQ |
|---|---|---|
| In-mold labeling | Full-color graphics with 3D effect | 5,000 units |
| Hot stamping | Metallic logo application | 3,000 units |
| Screen printing | Multi-color branding | 1,000 units |
Industry Applications
The company’s containers serve multiple sectors with specialized solutions:
Chemical Industry
UN-certified buckets with chemical-resistant liners safely store solvents, adhesives, and cleaning agents. The double-wall construction provides secondary containment for hazardous liquids, while color-coding systems prevent cross-contamination in production facilities.
Agricultural Sector
UV-stabilized fertilizer buckets feature measurement markings and easy-pour spouts. The antimicrobial treatment prevents bacterial growth in bio-fertilizer applications, extending product shelf life by up to 40% compared to standard containers.
Food Processing
FDA-compliant containers with tamper-evident seals ensure product integrity during transport. The airtight design maintains freshness for powdered ingredients, while the translucent material allows inventory checks without opening containers.
Quality Assurance System
The ISO 9001:2015 certified facility implements a six-layer quality control system:
- Raw material inspection with spectrometric analysis
- In-process monitoring using statistical process control
- 100% dimensional verification with CMM machines
- Random sampling for performance testing
- Final inspection before packaging
- Batch traceability through QR code labeling
The on-site laboratory conducts 28 different tests including drop impact, stack load, and chemical compatibility assessments. All test reports are archived for five years, enabling complete product traceability throughout the supply chain.
FAQ
What customization options are available for plastic buckets?
We offer comprehensive customization including material selection (HDPE/PP/LDPE), capacity from 5L to 50L, UN certification for hazardous materials, and multiple branding methods like in-mold labeling and hot stamping. Our engineering team can also develop specialized features such as tamper-evident seals and ergonomic handles.
How does your quality control system ensure product reliability?
Our ISO 9001:2015 certified facility implements six-layer quality control including raw material spectrometric analysis, in-process statistical monitoring, 100% dimensional verification, random performance testing, final inspection, and batch traceability. Each container undergoes 28 different tests in our on-site laboratory.
What certifications do your plastic buckets hold?
Our products comply with FDA food safety standards, EU REACH regulations, and UN transportation requirements for hazardous materials. We provide SGS test reports for chemical resistance, UV stability, and impact resistance. All certification documents are available for customer verification.
How do you handle large-volume orders with short lead times?
With 24 fully automated production lines and 120,000 units monthly capacity, we maintain standard product stock for immediate shipment. For custom orders, our modular production system allows parallel processing of different components, reducing lead times by 30% compared to traditional manufacturing methods.
What environmental protection measures do you implement?
We use 100% recyclable materials and operate a closed-loop water recycling system that reduces consumption by 65%. Our production process generates zero industrial waste, with all plastic scrap being reground and reused. We also offer biodegradable additive options for customers seeking eco-friendly solutions.
Summary
Hejian Haoyun Plastic Factory has established itself as a global leader in custom injection-molded plastic bucket manufacturing through its commitment to quality, innovation, and customer service. The company’s vertically integrated production system, combining advanced automation with precision engineering, enables cost-effective delivery of durable, customized containers that meet the stringent requirements of diverse industries. With a focus on continuous improvement and sustainable practices, Hejian Haoyun remains dedicated to providing reliable packaging solutions that help clients enhance operational efficiency and brand value worldwide.