
In the global industrial packaging market, finding reliable manufacturers of high-quality plastic containers remains a critical challenge for buyers. Hejian Haoyun Plastic Factory, located in Hejian City, Hebei Province, has established itself as a leading producer of 5L-25L full-specification plastic buckets through advanced manufacturing capabilities and customer-centric services. Covering an area of 5,000 square meters, our modern factory combines international-standard production facilities with a comprehensive quality management system to deliver packaging solutions that meet diverse industry requirements.
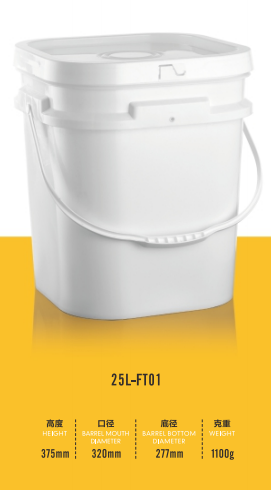
Comprehensive Product Range for Industrial Applications
Our core product portfolio includes six specialized plastic bucket categories designed for specific industry needs: waterproof coating buckets, fireproof coating buckets, agricultural fertilizer buckets, biological agent buckets, pesticide buckets, and car wash liquid buckets. Each product line undergoes rigorous material selection and structural design to ensure optimal performance in demanding environments.
The 5L-25L capacity range addresses both small-scale operational needs and bulk storage requirements. Our 5L buckets prove ideal for premium biological agents and concentrated pesticides, while the 25L variants efficiently handle large-volume agricultural chemicals and industrial coatings. The graduated sizing options enable customers to select containers that maximize storage efficiency while maintaining proper product-to-container ratios.
Material composition plays a crucial role in our product design. We utilize high-density polyethylene (HDPE) and polypropylene (PP) as primary materials, both known for their exceptional chemical resistance, impact strength, and temperature tolerance. These materials maintain structural integrity when storing corrosive substances like industrial solvents, agricultural chemicals, and cleaning agents, ensuring long-term product protection and user safety.
Advanced Manufacturing Capabilities
Our production infrastructure represents the convergence of automation technology and precision engineering. The factory houses 12 state-of-the-art injection molding machines with clamping forces ranging from 280 to 1,200 tons, enabling simultaneous production of multiple container sizes with consistent quality. The fully automated production lines integrate material feeding, molding, cooling, and ejection processes, achieving daily output capacities exceeding 20,000 units while maintaining ±0.5mm dimensional accuracy.
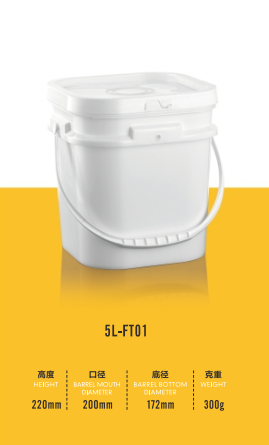
The precision mold workshop occupies 1,200 square meters of dedicated space, housing CNC machining centers and EDM equipment capable of producing molds with complex geometries and micro-structures. Our mold design team incorporates finite element analysis (FEA) to optimize container wall thickness distribution, ensuring maximum strength with minimal material usage. This engineering approach results in buckets that withstand 1.5-meter drop tests without deformation or leakage.
Quality control permeates every production stage through our ISO 9001:2015 certified management system. Raw material batches undergo comprehensive testing for density, melt flow index, and chemical resistance before entering production. During molding, real-time monitoring systems track cavity pressure, cooling time, and ejection force parameters. Finished products pass through automated inspection stations equipped with high-resolution cameras and laser scanners to detect surface defects, dimensional variations, and sealing integrity issues.
Customization Services for Brand Enhancement
Understanding the importance of brand identity in competitive markets, we offer comprehensive customization services through three primary decoration technologies:
- In-Mold Labeling (IML): This process embeds pre-printed labels directly into the mold cavity during injection, creating seamless integration between container and decoration. IML offers superior scratch resistance and moisture protection compared to traditional labeling methods, making it ideal for chemical products requiring long shelf lives.
- Hot Stamping: For premium packaging applications, our hot stamping equipment applies metallic foil logos and patterns with micron-level precision. This technique creates eye-catching, durable branding elements that withstand handling and environmental exposure.
- Screen Printing: Our six-color screen printing lines produce vibrant, multi-color graphics with excellent opacity on both transparent and colored containers. This method proves particularly effective for displaying product information, safety warnings, and usage instructions in multiple languages.
The customization process begins with our professional design team, which collaborates with clients to translate branding concepts into production-ready artwork. Using 3D modeling software, we create virtual prototypes that simulate final product appearance, enabling clients to evaluate design elements before committing to production. This iterative approach minimizes development time while ensuring complete satisfaction with the finished packaging.
| Customization Parameter | Available Options |
|---|---|
| Capacity Range | 5L, 10L, 15L, 20L, 25L (custom sizes available) |
| Color Selection | Standard colors (white, blue, black) + Pantone matching |
| Decoration Methods | In-mold labeling, hot stamping, screen printing |
| Closure Options | Screw cap, tamper-evident cap, child-resistant cap |
| Material Grade | Food-grade, chemical-resistant, UV-stabilized |
Industry-Specific Packaging Solutions
Our engineering team develops specialized container designs to address unique challenges across different sectors:
Agricultural Chemical Packaging: For pesticide and fertilizer applications, we produce buckets with reinforced sidewalls and integrated handles designed to withstand rough handling in field environments. The containers feature double-wall construction in critical areas to prevent accidental puncturing, while the sealing systems incorporate EPDM gaskets that maintain chemical resistance across a wide pH range.
Coating Industry Solutions: Waterproof and fireproof coating containers require specific design considerations to prevent product degradation. Our solutions include UV-stabilized materials that protect light-sensitive formulations, along with conical bucket designs that facilitate complete product discharge during application. The smooth interior surfaces minimize coating residue buildup, reducing waste and cleaning requirements.
Daily Chemical Packaging: Car wash liquid and detergent containers must balance chemical resistance with aesthetic appeal. We produce translucent buckets that allow visual product level monitoring, combined with ergonomic handles that ensure comfortable handling during dispensing. The containers undergo stress-crack resistance testing to guarantee performance when storing surfactant-based formulations.
Food Processing Applications: Our food-grade buckets comply with FDA regulations and EU 10/2011 standards for plastic materials in contact with food. The production environment maintains HACCP-certified cleanroom conditions, with regular microbial testing of both materials and finished products. These containers feature smooth, crevice-free interiors that facilitate thorough cleaning and sanitization between uses.
FAQ
What certifications do your plastic buckets hold for international markets?
Our products comply with multiple international standards including ISO 9001:2015 for quality management, FDA regulations for food contact materials, and REACH/RoHS for chemical safety. For specific markets, we provide UN-approved packaging solutions that meet Dangerous Goods Transportation requirements, along with GMP certification for pharmaceutical-grade containers.
How does your factory ensure consistent product quality across large orders?
Quality control begins with raw material batch testing and continues through every production stage. Our automated systems monitor key parameters in real-time, while statistical process control (SPC) methods track quality trends. Each production run includes samples tested for drop resistance, sealing integrity, and chemical compatibility before bulk shipping.
What is your minimum order quantity for custom-designed buckets?
The MOQ varies based on customization complexity. For standard containers with basic labeling, we accept orders starting from 1,000 units. Fully custom designs involving new mold development typically require minimum orders of 5,000-10,000 units, depending on container size and decoration requirements. We offer free sample production for design verification before full-scale manufacturing.
How do you handle urgent orders or short delivery timelines?
Our production planning system maintains dedicated capacity for priority orders. With 12 injection molding machines operating simultaneously, we can allocate specific equipment to urgent projects. For port direct delivery clients, we stock standard container models in our warehouse for immediate shipment, with customization services available for subsequent orders.
Summary
Hejian Haoyun Plastic Factory has positioned itself as a comprehensive solution provider in the industrial plastic packaging sector through technical innovation and customer-focused services. Our 5,000-square-meter facility combines advanced manufacturing equipment with rigorous quality control systems to produce 5L-25L plastic buckets that meet diverse industry requirements. The product range covers specialized containers for agricultural chemicals, industrial coatings, daily chemicals, and food processing applications, all available with extensive customization options.
The factory’s competitive advantages stem from its vertical integration capabilities, from precision mold making to automated mass production. This structure enables us to maintain strict control over product quality while offering flexible customization services. Our commitment to sustainable manufacturing practices, including material recycling programs and energy-efficient production processes, aligns with global environmental standards and customer expectations for responsible sourcing.
With a professional team of engineers, quality inspectors, and customer service specialists, we provide end-to-end support from initial design consultation to after-sales service. The port direct delivery model optimizes shipping efficiency for international clients, while our free sampling policy and OEM labeling services facilitate brand development without significant upfront investment. As the industrial packaging market continues to evolve, Hejian Haoyun remains dedicated to advancing plastic container technology and delivering value-added solutions to global partners.